
Book a demo
Tell us about your nanoparticle or RNA project and request Ntensify® micro and mini demo
Our team will get back to you shortly to schedule your session.
Contact
Any inquiries about RNA synthesis systems?
Drop us a line!
Contact
Any inquiries about your nanoparticle/RNA-LNP formulation?
Drop us a line!
Contact
Any inquiries about your nanoparticle/RNA-LNP formulation?
Drop us a line!
Book a demo
Tell us about your nanoparticle or RNA-LNP project and request a TAMARA demonstration.
Our team will get back to you shortly to schedule your session.
MICROFLUIDICS
Microfluidic mixing for precise control of RNA-LNP formulation, across R&D from the very first microliter
Designed to reproduce the same mixing conditions run after run, for controlled, uniform, optimally encapsulated RNA-LNPs even at very small volumes.


Control and reproduce LNP characteristics (size, PDI…) through flow conditions while maximizing encapsulation efficiency
Ideal for screening and preclinical work, up to tens of milliliters per run
Efficient laminar mixing set by channel geometry and flow rates, even at the smallest volumes
Controlled mixing is part of your RNA-LNP
RNA-LNP formation is driven by self-assembly of the lipids around the RNA, happening within milliseconds after the organic and aqueous phases meet in the fluidic mixer. How fast and how evenly they mix sets size, PDI, encapsulation, internal structure and more… and through them how the particle behaves in cells and in vivo [1,2].
In development work, this has three practical consequences:
- If mixing varies from run to run, a difference in biological outcome between two formulations may come from the process rather than from the formulation itself.
- Conversely, once mixing is controlled, it becomes a lever: flow conditions can be tuned to adjust size, PDI and encapsulation, and with them RNA-LNP performance.
- If the process loses material, you pay for it in RNA and lipids, the scarcest inputs at this stage.
Microfluidic mixing answers the first. By replacing pipetting and vortexing with defined, continuously controlled flow, it has become the gold-standard method for RNA-LNP research and preclinical development. The second depends on how the fluidic system handling around the mixer is designed.

Figure 1 – The formulation method is one critical process parameter among several. Change it, and the quality attributes can change with it.
Laminar mixing drives microfluidic nanoparticle formulation
Flow in microchannels is typically laminar. In simple channel geometries, mixing therefore relies largely on slow molecular diffusion. Advanced micromixer geometries can enhance mixing by generating secondary flows and chaotic advection, increasing interfacial contact between the two phases hence maximizing mixing speed and efficiency. [3].
Different micromixers, one principle
Diffusion-dominated designs, such as T- and Y-junctions or hydrodynamic flow focusing, rely primarily on molecular diffusion, which limit mixing efficiency. To achieve more efficient mixing, chaotic designs use engineered channel geometries to repeatedly stretch and fold the fluid interface to maximize the surface exchange between the 2 liquids. Several chaotic geometries commonly used for LNP formulation:
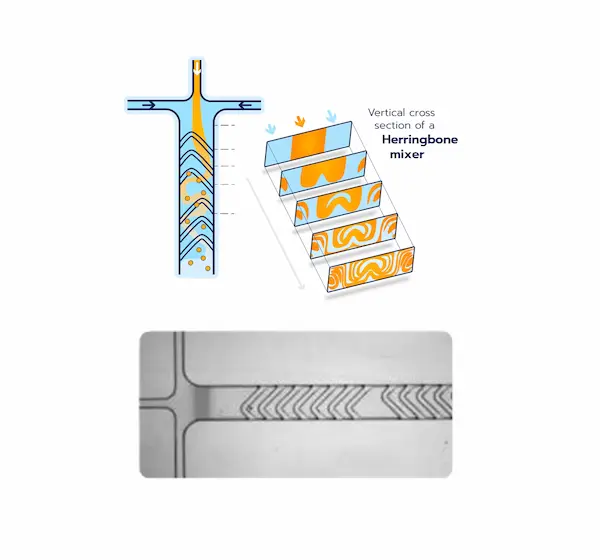
- Staggered herringbone mixer — asymmetric grooves on the channel floor generate transverse flows that fold the two phases over each other in three dimensions [3].
- Baffle mixer — periodic turns along a two-dimensional channel create secondary flows that repeatedly stretch and fold the interface [4].
Whatever the design, the logic is the same: geometry and flow rates set the mixing time, and the mixing time shapes the particle. For a detailed overview of micromixer designs, see our review on the fundamentals of microfluidic mixing for LNP synthesis.
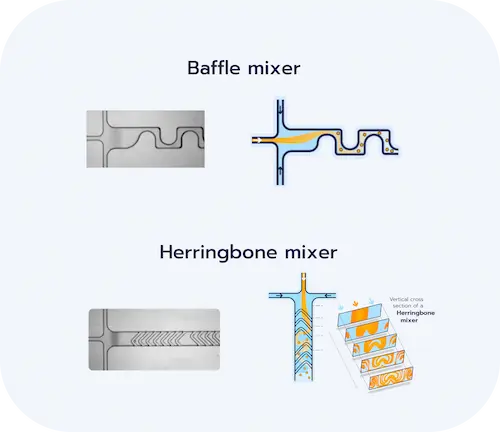
Figure 2 – Two chaotic micromixer geometries: a baffled mixer (top) and a staggered herringbone mixer (bottom)

Fast mixing
Rapid mixing drives fast ethanol dilution and solvent exchange, creating controlled conditions for lipid self-assembly and favoring small, homogeneous particles with high encapsulation efficiency.

Reproducible mixing
The mixing conditions are set by channel geometry and flow rates. Keeping them consistent ensures the same mixing conditions, hence identical RNA-LNP run after run.
Controlling nanoparticle formation
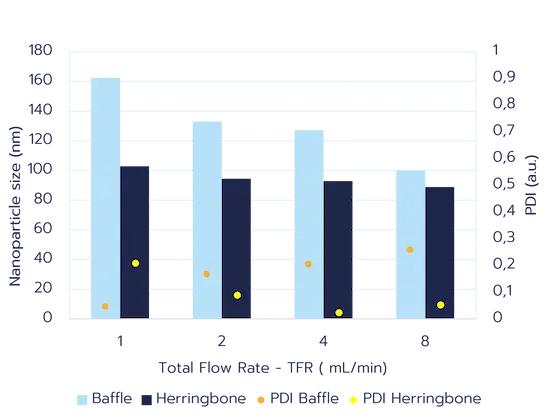
Figure 3 – Influence of TFR and mixer influence on LNP size & PDI
Total flow rate (TFR) — main lever on particle size; higher TFR, faster mixing, smaller LNPs.
Flow rate ratio (FRR) — sets the aqueous-to-organic ratio and how fast the solvent is diluted; a higher FRR generally gives smaller particles.
Mixer geometry — sets how quickly the two phases fold together at a given flow rate.
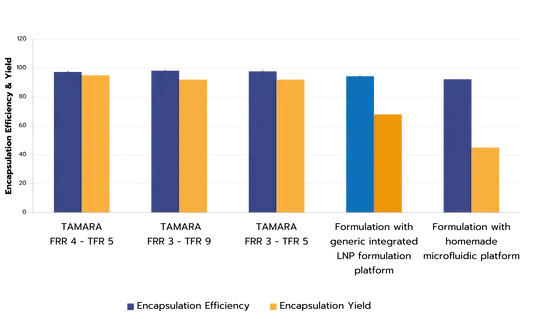
Figure 4 – Comparison of EE% and EY% in both an optimized lossless platform (TAMARA), a generic integrated microfluidic formulation system, and a typical homemade system
What encapsulation yield shows that encapsulation efficiency doesn’t
Encapsulation efficiency (EE%) answers a formulation quality question: of the RNA in your final sample, how much is inside particles? A low EE% means loads of free RNA which reduce payload delivery and may contributes to toxicity.
Encapsulation yield (EY%) answers a process question: of the RNA you started with, how much ended up encapsulated in your sample?
Because EE% is a ratio measured inside the vial, it is blind to everything that never reached the vial: RNA left in dead volumes, head and tail fractions discarded at each run, liquid held up in tubing or cartridges, material lost during purification. Two processes can both report 95% EE% while one recovers 90 µg of encapsulated RNA from a 100 µg input and the other only 60 µg.
That gap shows where RNA is scarce: fewer conditions screened per milligram of RNA, lower doses reachable at a given volume, a higher real cost per formulation. Pipette mixing, for instance, loses little material because it has no fluidic path. A microfluidic system only matches that if its own fluidic path is designed to avoid losses: under optimal conditions, such a design reaches EY% above 90%. Run time counts too, as very short runs at the smallest volumes can lower EY%.
The mixing principle does not set EY% on its own; the fluidic system around the mixer and the downstream steps do. Report both values. More in our guide to choosing an LNP formulation system.
Microfluidic mixing vs hand mixing
A practical comparison of microfluidic’s efficacy is comparing it with hand mixing. Hand mixing, where the ethanolic lipid phase is pipetted into the aqueous RNA phase, is still widely used in early research. It is accessible and works at very low volumes. What it cannot do is define the mixing.
Table 1 – Hand mixing and microfluidic mixing for LNP formulation.
| Hand mixing | Microfluidic mixing | |
|---|---|---|
| Equipment | A pipette | A dedicated microfluidic system |
| Mixing kinetics | Slow and poorly defined, with local concentration gradients | Milliseconds, under defined flow conditions |
| Size control | Limited: mixing time and energy cannot be set – LNP are usually larger | Tunable through TFR and FRR |
| Encapsulation Efficiency | Medium (~70%) | Highest (>95%) |
| Operator dependency | Strong (pipetting speed, injection angle) | Minimal |
| Volumes | Very low volumes; hard to extend to in vivo quantities | From very low volumes to in vivo-relevant quantities |
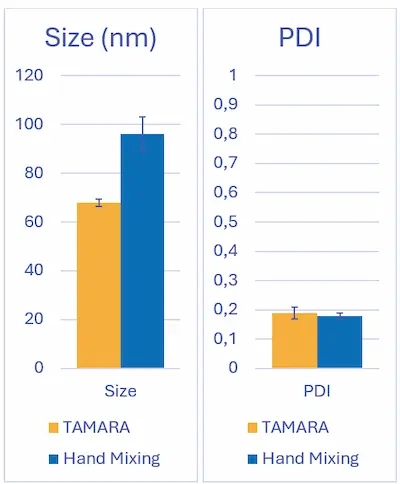
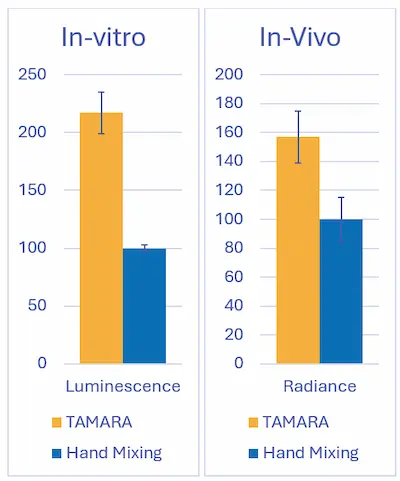
Figure 5 – LNP made by hand mixing vs microfluidic mixing, same ALC-0315-based formulation.
In a head-to-head study with Kurt Ristroph’s team at Purdue University (see [1] and Fig. 4), the same ALC-0315-based formulation (FRR 3:1, N/P 5, triplicates) was prepared by hand mixing and with a staggered herringbone micromixer, the mixing method being the only variable.
All physicochemical parameters – but the PDI – got impacts, and so did the biology. The difference came from size and from subtler features set during mixing, such as internal structure and population homogeneity, which population-averaged measurements capture only partly. The mixing method belongs in the methods section with the same rigor as the lipid composition. Full data in our review on hand mixing vs microfluidic mixing.
Where microfluidic mixing stops
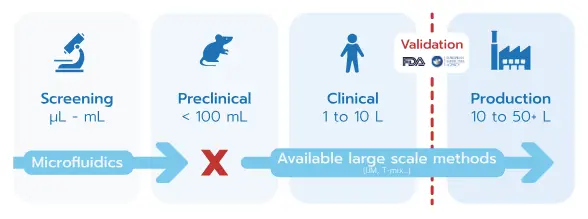
Microfluidic mixing gives its finest control at research and preclinical volumes, from microliters to tens of milliliters per run, and allows for high efficiency in screening RNA, Lipids compounds…
Beyond it however, 2 main limitations appear:
1/ throughput: By nature microfluidic channels remains of small dimensions and thus do not allow for high flow rates
2/ During extended operation, particle deposition or LNP’s natural tendency to agglomerate on microchannels walls lead to fouling and eventually to partial or complete channel blockage after a 10s to 100s of mL of formulation
In practice, parallelizing has often been explored but remain an near impossible engineering challenge as any – even partial – clogging lead to flow imbalance, impacting all the other channels.
In practice, microfluidics becomes impractical over a few 100s of mL of formulations, hence clinical-scale production typically relies on other approaches such as turbulent mixers [5] or our NanoPulse technology (which also ensures identical mixing hence LNP from screening to production)
Microfluidic mixing on your bench, with TAMARA
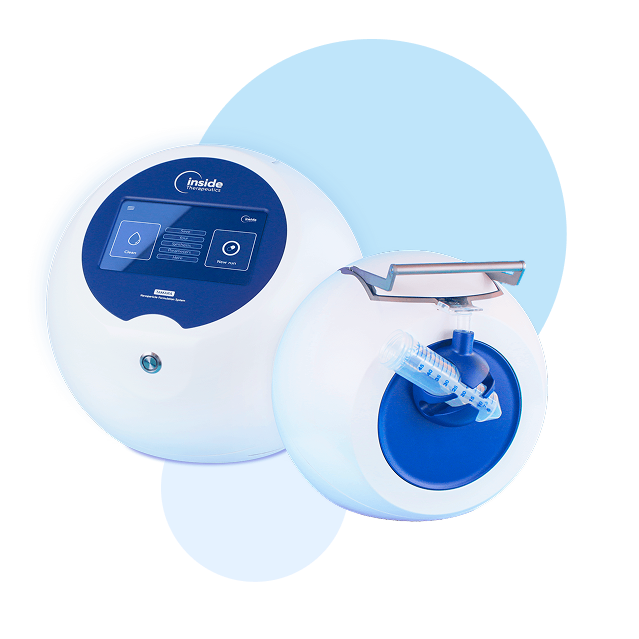
TAMARA® is our microfluidic formulation platform, built around the principles on this page:

Intuitive and quick
Save time in the lab — even for first-time users.
One system from screening to in vivo
0.2 to 30 mL per run, 1 µg to 5 mg of RNA
Lossless
No head-and-tail losses, with EY% above 90% under optimal conditions
Flexible mixing designs
Staggered herringbone and baffle mixers on one reversible, reusable chip
References
[1] T. Bethiana et al., “Identifying differential effects from eleven mixing techniques on mRNA lipid nanoparticle physicochemistry and biological performance,” bioRxiv, Nov. 09, 2025, doi: 10.1101/2025.11.07.687311.
[2] Y. Mo and G. Zheng, “From Morphology to Mechanism: Cryo-Electron Microscopy Insights into Lipid Nanoparticles for RNA Delivery,” ACS Nano, vol. 20, no. 28, pp. 19906–19929, Jul. 2026, doi: 10.1021/acsnano.6c09354.
[3] A. D. Stroock, S. K. W. Dertinger, A. Ajdari, I. Mezić, H. A. Stone, and G. M. Whitesides, “Chaotic mixer for microchannels,” Science, vol. 295, no. 5555, pp. 647–651, Jan. 2002, doi: 10.1126/science.1066238.
[4] N. Kimura, M. Maeki, Y. Sato, Y. Note, A. Ishida, H. Tani, H. Harashima, and M. Tokeshi, “Development of the iLiNP device: fine tuning the lipid nanoparticle size within 10 nm for drug delivery,” ACS Omega, vol. 3, no. 5, pp. 5044–5051, May 2018, doi: 10.1021/acsomega.8b00341.
[5] P. L. Ahl, “Microfluidic and turbulent mixing for mRNA LNP vaccines,” Pharmaceutics, vol. 17, no. 9, p. 1148, Sep. 2025, doi: 10.3390/pharmaceutics17091148.
Ready to use microfluidics for LNP formulation?
Book your personalized demo or talk to one of our experts!
Response within 24 hours. Your data is secure & never shared